






Open die forging double acting press UZTM 4654 — 6600 ton
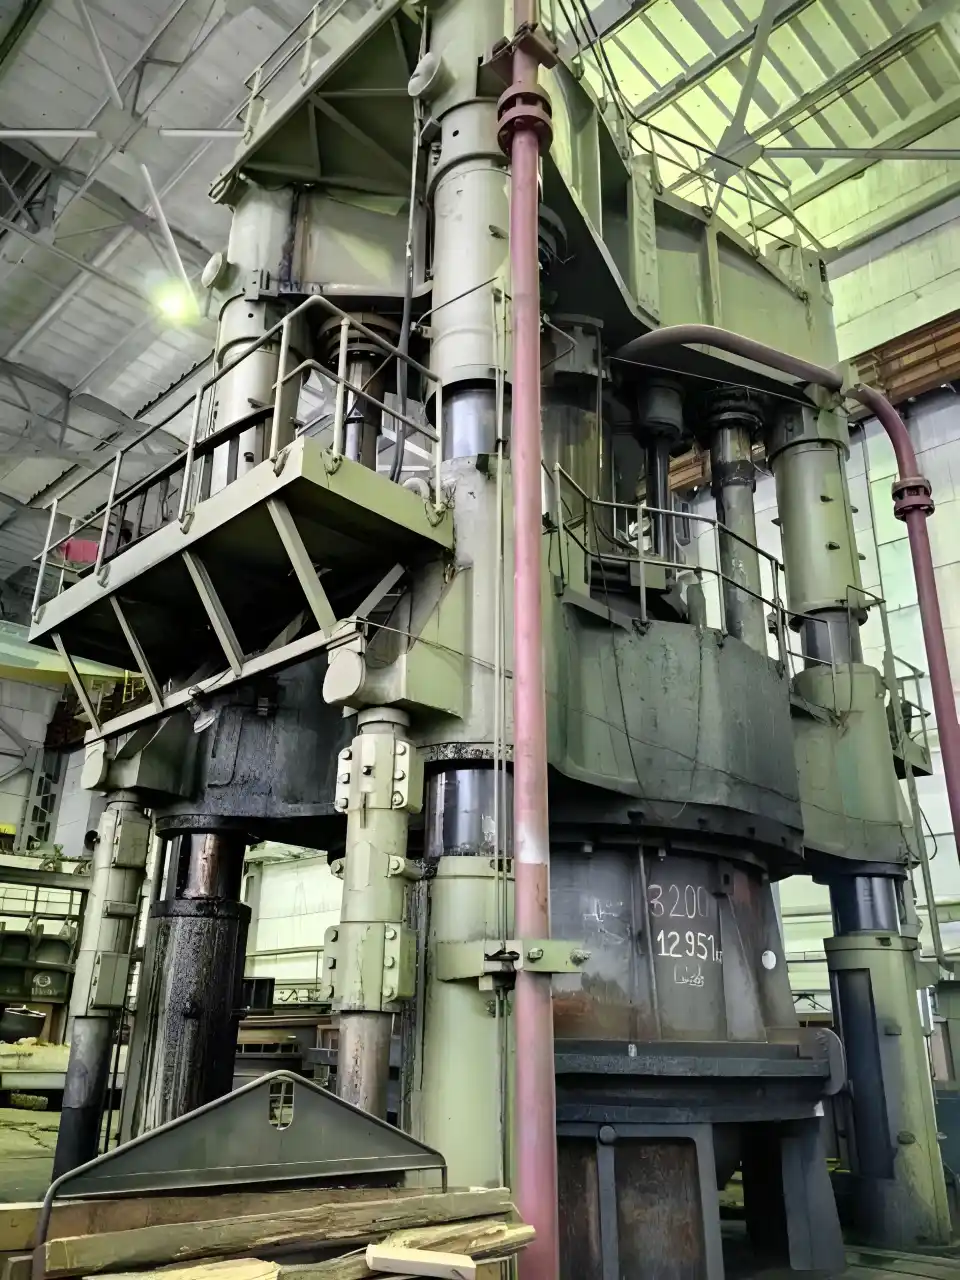


UZTM 4654 open die forging press - description
Technical specifications UZTM 4654 (ID:76523)
| Type | Open die forging press |
|---|---|
| Manufacturer | UZTM |
| Model | 4654 |
| Nominal force | 66000 kN / 6600 ton |
| Main slide force | 42000 kN / 4200 ton |
| Clamping slide force | 24000 kN / 2400 ton |
| Table size | 4200 x 6000 mm |
| Main slide stroke | 2500 mm |
| Clamping slide stroke | 1250 mm |
| Moving table stroke | 5750 mm |
| Minimum daylight ram down | 3750 mm |
| Distance between columns | 2620 x 4970 mm |
| Columns diameter | 630 mm |
| Max workpiece weight | 100000 kg / 100 ton |
| Weight | 1061000 kg |
Please note: Specifications are indicative and subject to final confirmation. For current availability and price, as well as photos and technical details, please contact us.
Open die forging press UZTM - technological processes and operations
| Forging | The process of plastic deformation of metal, in which the workpiece changes shape under the impact of blows or static pressure. During forging, the metal structure is densified, internal inhomogeneities are eliminated, and the mechanical properties of the material are improved. As a result, forged products are distinguished by high strength and reliability when operating under significant loads. Forging is used both for producing finished parts and for preparing workpieces for subsequent stamping. |
|---|---|
| Hot forging | Hot forging is a process of shaping metal under pressure at elevated temperatures. Heating reduces the deformation resistance of the material, allowing it to flow more easily into the die cavity. The process provides high productivity and the ability to form complex shapes. Used for manufacturing forgings from steel and alloys in series and mass production. |
| Open-die forging | Metal is deformed between flat or shaped tools without lateral restriction, allowing free flow in all directions. The workpiece is gradually shaped by repeated blows or press strokes, with the operator controlling its position between each step. This method is used for producing large forgings such as shafts, discs, and rings, where a refined internal structure is essential. |
| Preforming | Preforming prepares the workpiece for the main stamping operation by giving it an approximate shape of the future part. The metal is distributed in the die to facilitate final filling and reduce tool wear. This intermediate step improves accuracy and quality of the finished product. |
| Piercing | Piercing forms a hole in a solid workpiece by driving a tool through the material without removing it. The metal is displaced sideways, creating a through or blind opening while preserving the structure around it. The operation is performed on presses and is used in the production of hollow parts such as bushings, rings, and shafts. |