
Mechanical press Stanko KM2134A — 250 ton
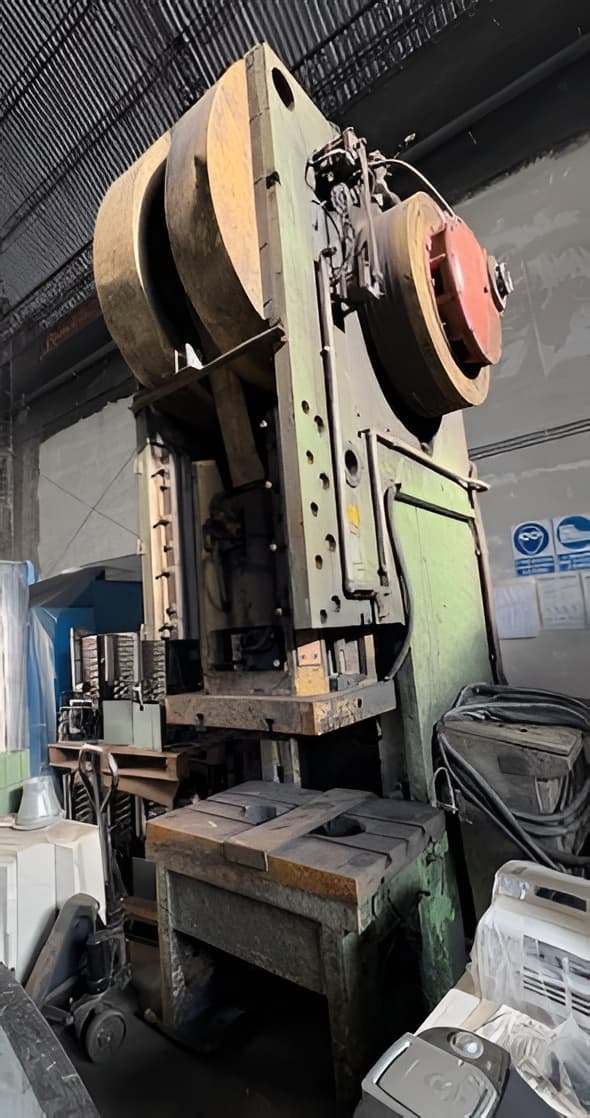
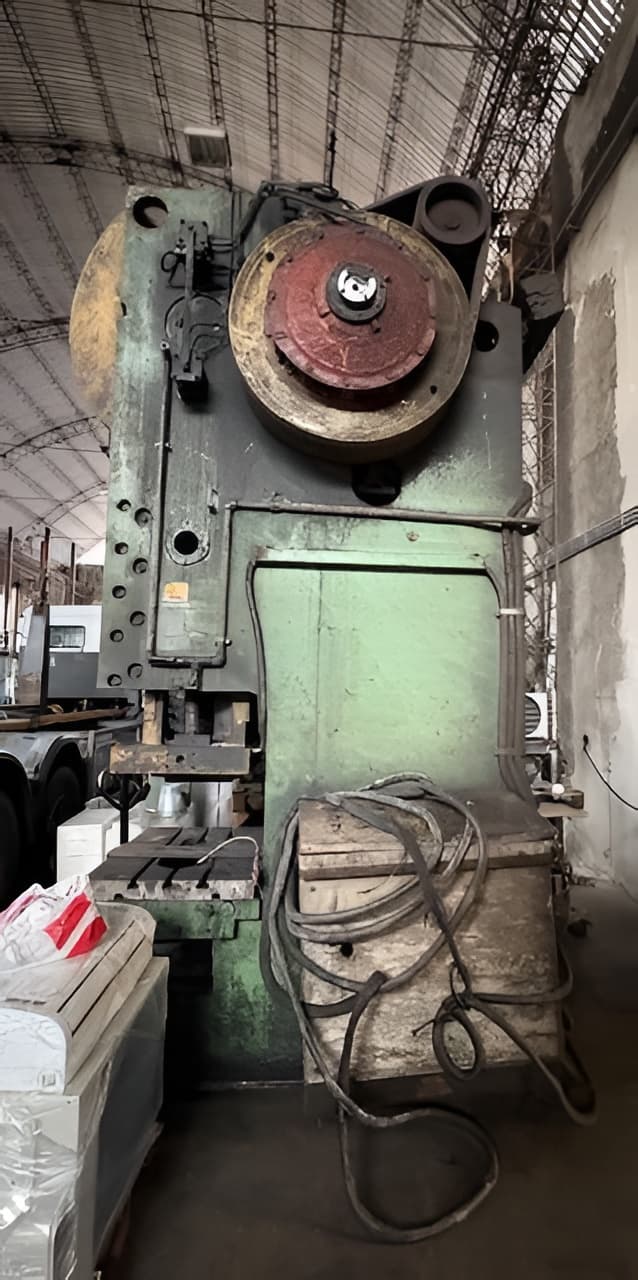
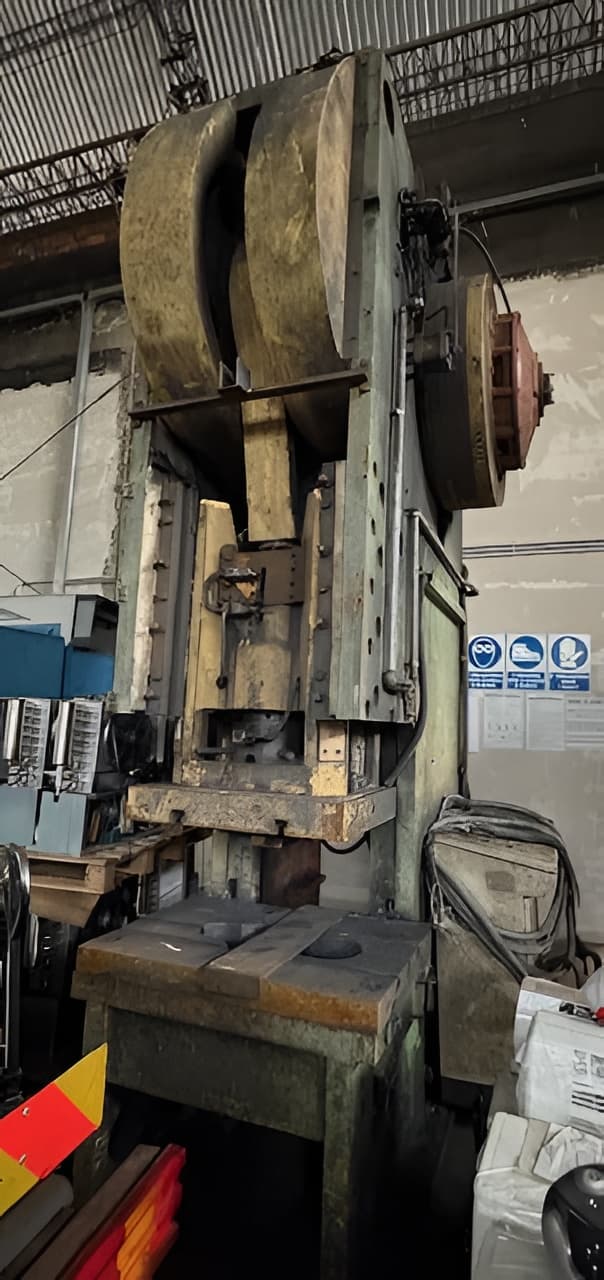
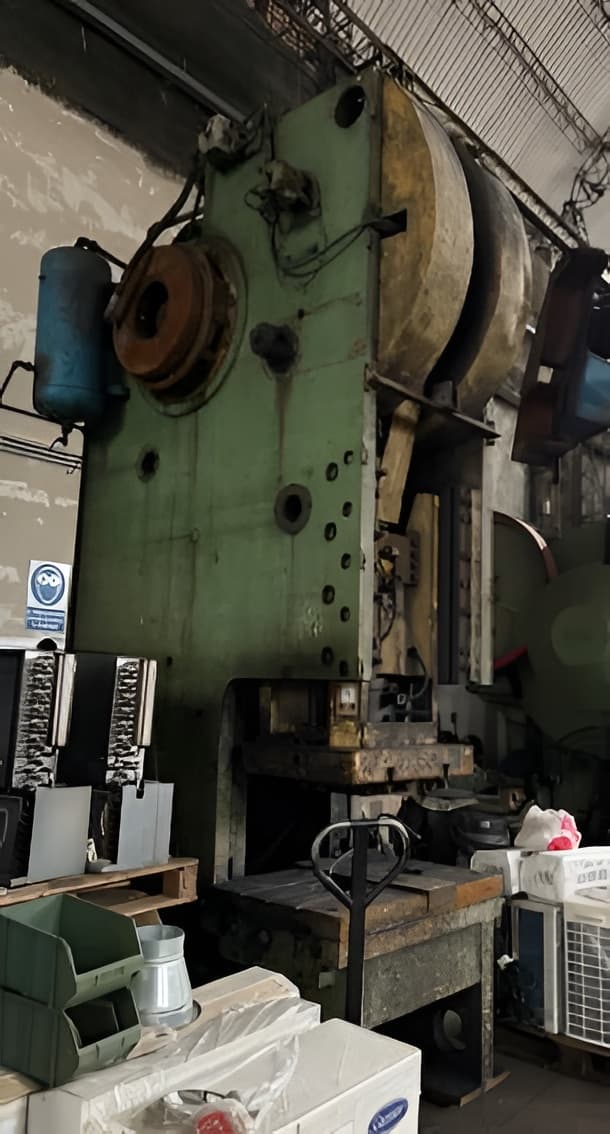
Stanko KM2134A c-type press - description
Technical specifications Stanko KM2134A (ID:76538)
| Type | C-type press |
|---|---|
| Manufacturer | Stanko |
| Model | KM2134A |
| Nominal force | 2500 kN / 250 ton |
| Adjustable ram stroke | 25–200 mm |
| Ram adjustment | 140 mm |
| Strokes per minute continuous | 61 |
| Strokes per minute single | 25 |
| Table size | 1120 x 750 mm |
| Main motor power | 25 kW |
| Overall dimensions approx. | 2500 x 2700 x 4200 mm |
| Total weight | 21500 kg |
Please note: Specifications are indicative and subject to final confirmation. For current availability and price, as well as photos and technical details, please contact us.
C-type press Stanko - technological processes and operations
| Trimming | When a hot forging leaves the die, flash comes out with it — excess metal squeezed into the gap between the tools. It is removed on a trimming press, where the part passes through a die and the cutting edge shears off everything excess along the contour. This is how the forging gets a clean edge and precise shape, ready for the next stage. |
|---|---|
| Sheet stamping | Sheet stamping is a class of operations for forming parts from sheet material using dies. The workpiece is deformed in the tool without significant change in thickness, acquiring the specified shape. This group includes blanking, punching, bending, drawing, and other processes performed on presses. Sheet stamping is the foundation of mass production of body panels, housings, and other thin metal parts. |
| Drawing | Drawing turns a flat blank into a hollow product. The sheet is clamped at the edges while the tool presses the central part, forcing the metal to flow into the die cavity and form walls. This is how cups, caps, housings, and other parts with one open side are produced. |
| Punching | Punching holes in sheet metal is performed in a die: a tool with sharp edges passes through the workpiece, separating material along a closed contour. The process is fast and precise, leaving no burrs when properly set up. Used for producing holes, slots, and cutouts in sheet metal parts. |
| Blanking | Blanking a part from a sheet along a closed contour is performed on a press using a blanking die. The tool passes through the material, separating the finished part from the sheet. The accuracy of the contour and the cleanliness of the edge determine the quality of the final product. |
| Bending | Bending gives a sheet blank an angle or curvature. The metal is bent in the die under the force of the press: the outer layers stretch, the inner layers compress, and the middle retains its original length. The operation allows producing parts with the specified geometry without changing the material thickness. |
| Cutting | Separation of material into parts using a cutting tool. Depending on the task, cutting is performed on presses, shears, or special machines, separating the workpiece from a sheet, strip, or bar. The operation provides workpieces of the required size for subsequent forming. |