
Friction screw press SMS Hasenclever SPK 800/820/355/1075 — 800 ton
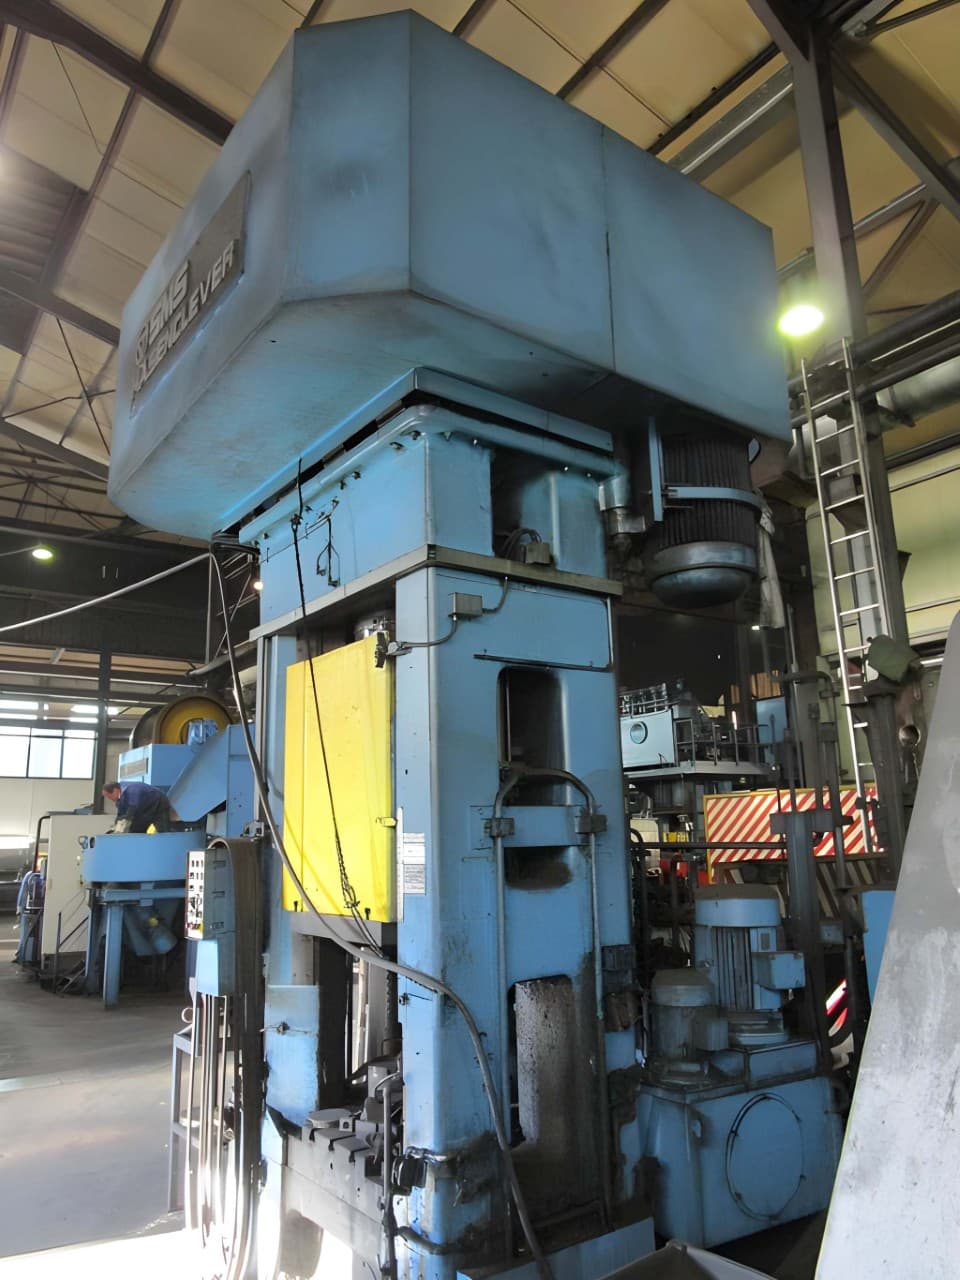
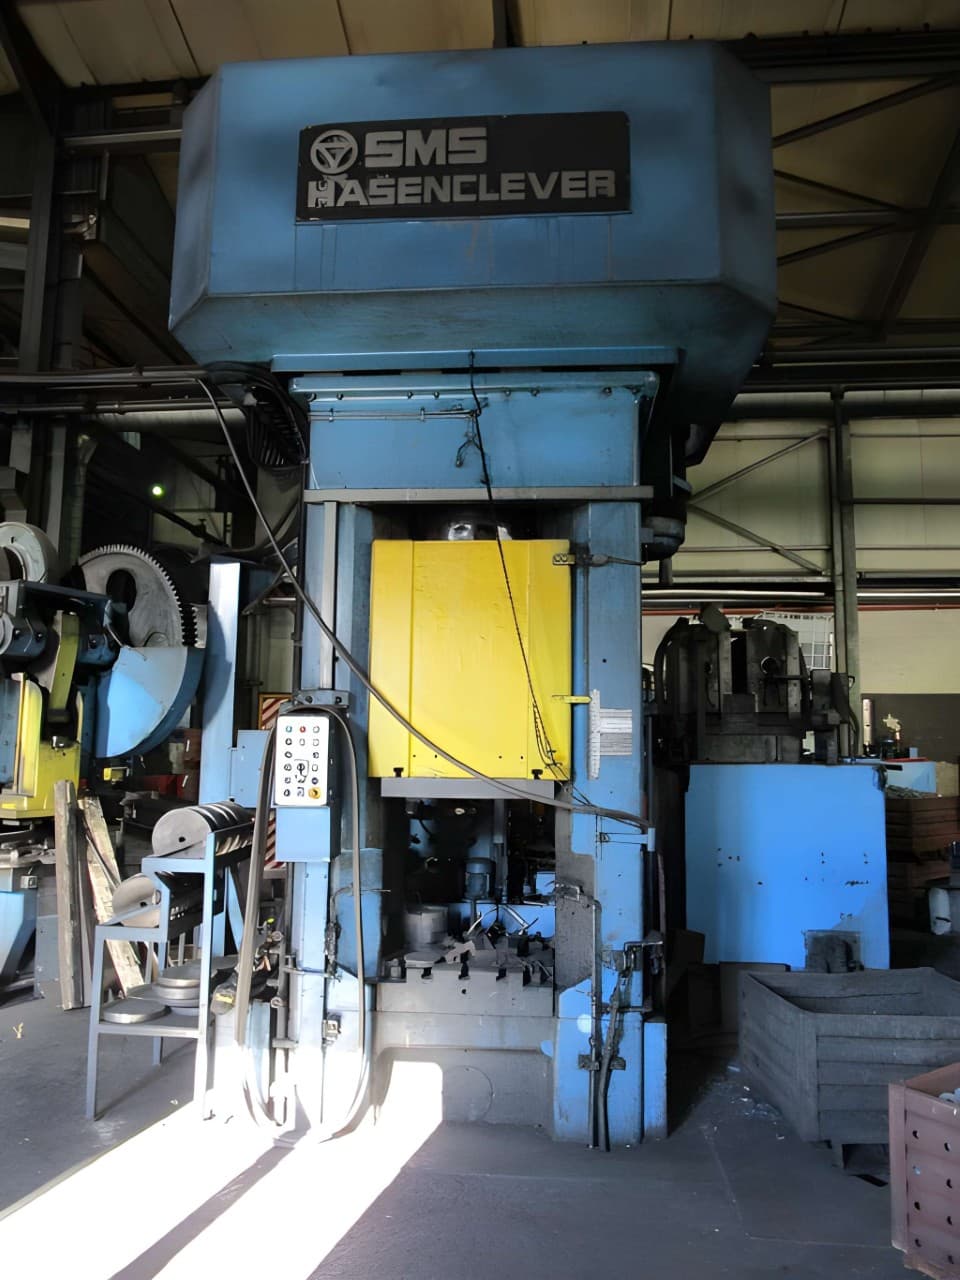
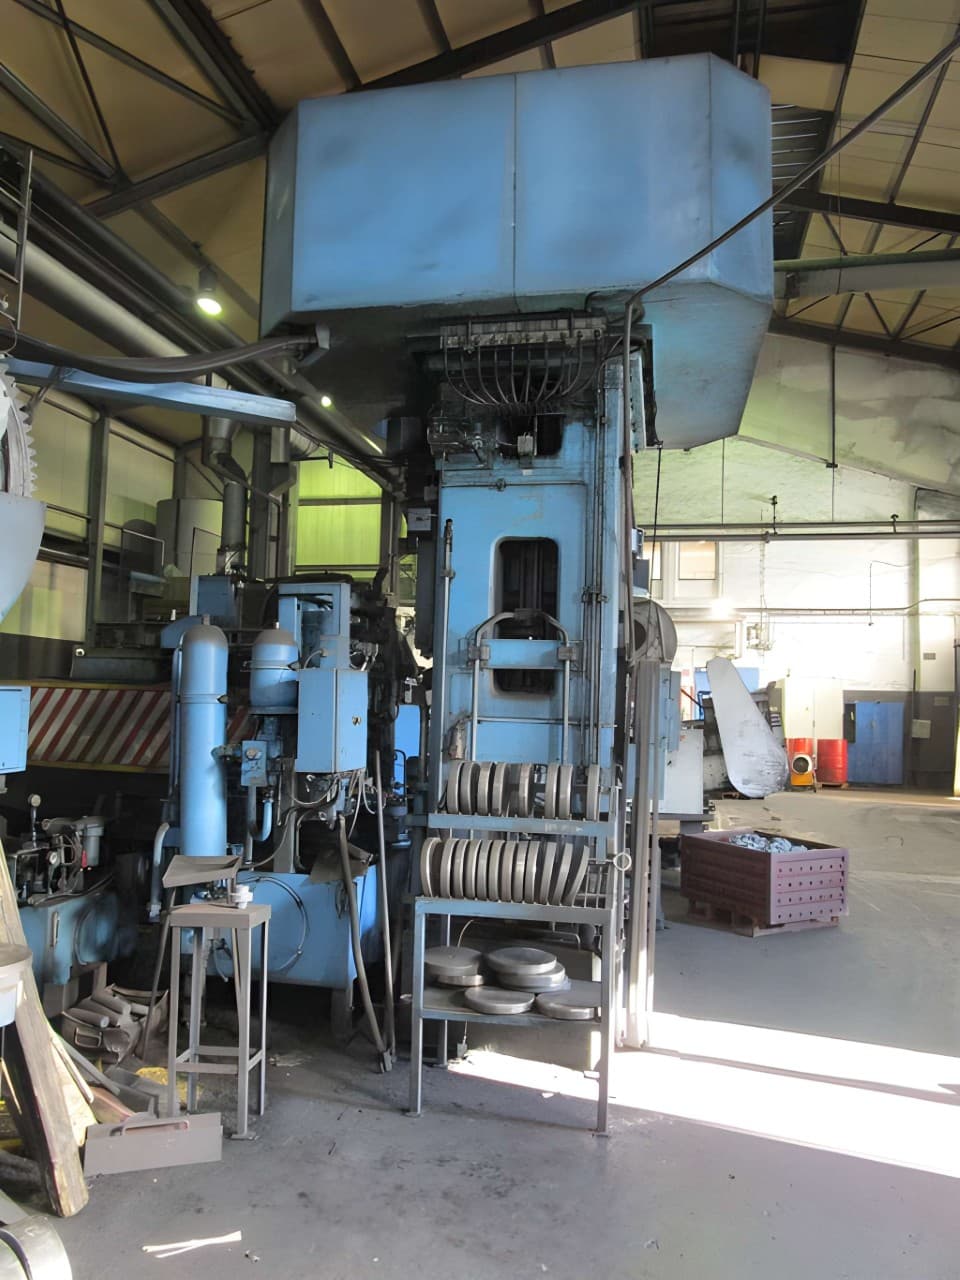
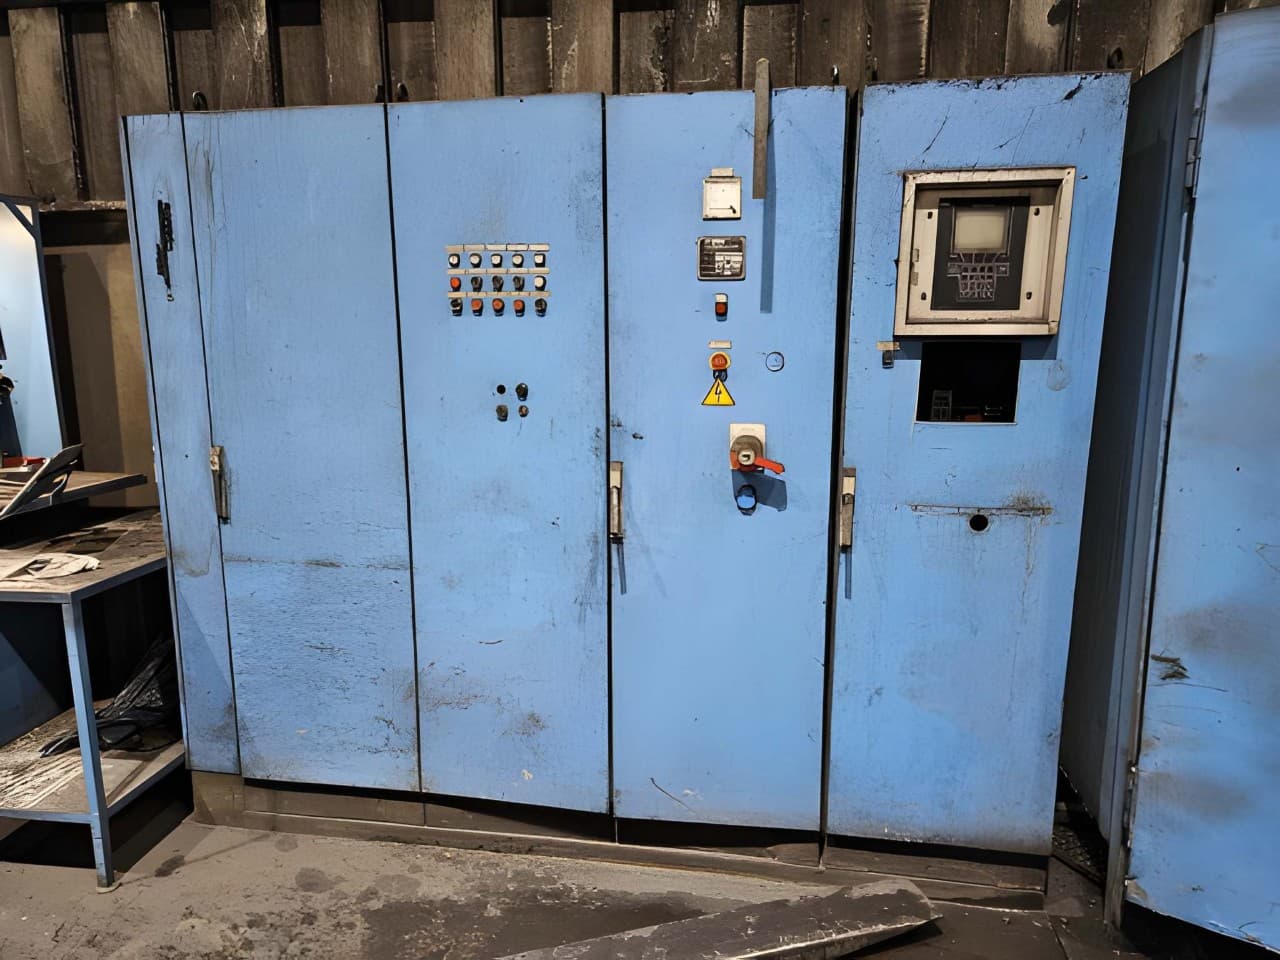
SMS Hasenclever SPK 800/820/355/1075 screw press - description
Technical specifications SMS Hasenclever SPK 800/820/355/1075 (ID:76546)
| Type | Screw press |
|---|---|
| Manufacturer | SMS Hasenclever |
| Model | SPK 800/820/355/1075 |
| Year of manufacture | 1991 |
| Nominal force | 8000 kN / 800 ton |
| Maximum permissible force | 10000 kN / 1000 ton |
| Useful energy at 15% flywheel speed drop | 100 kJ |
| Spindle diameter | 250 mm |
| Clear width between uprights | 820 mm |
| Table dimensions | 800 x 900 mm |
| Ram dimensions | 800 x 900 mm |
| Side window width | 315 mm |
| Maximum ram stroke | 355 mm |
| Minimum clear height | 720 mm |
| Ram speed | 0,53 m/s |
| Stroke cycle time | 1,7 s |
| Strokes per minute | 28–43 |
| Strokes per minute at 15% flywheel speed drop | 18 |
| Main motor power | 36 kW |
| Type designation | SPK 800/820/355/1075 |
| Mass | 30000 kg |
Please note: Specifications are indicative and subject to final confirmation. For current availability and price, as well as photos and technical details, please contact us.
Screw press SMS Hasenclever - technological processes and operations
| Forging | The process of plastic deformation of metal, in which the workpiece changes shape under the impact of blows or static pressure. During forging, the metal structure is densified, internal inhomogeneities are eliminated, and the mechanical properties of the material are improved. As a result, forged products are distinguished by high strength and reliability when operating under significant loads. Forging is used both for producing finished parts and for preparing workpieces for subsequent stamping. |
|---|---|
| Cold forging | Cold forging is a process of shaping metal under pressure at room temperature. The absence of heating provides high dimensional accuracy and a smooth surface finish. Due to work hardening, the finished parts acquire increased strength. The process is used for manufacturing precision parts with tight tolerances. |
| Hot forging | Hot forging is a process of shaping metal under pressure at elevated temperatures. Heating reduces the deformation resistance of the material, allowing it to flow more easily into the die cavity. The process provides high productivity and the ability to form complex shapes. Used for manufacturing forgings from steel and alloys in series and mass production. |
| Closed-die forging | The workpiece is deformed inside a die cavity that restricts metal flow, forcing it to fill the exact shape of the tool. Under high pressure, the material spreads into every recess and detail of the die, producing a part with precise geometry. This method provides high accuracy and repeatability, making it the standard for series and mass production of complex forgings. |
| Preforming | Preforming prepares the workpiece for the main stamping operation by giving it an approximate shape of the future part. The metal is distributed in the die to facilitate final filling and reduce tool wear. This intermediate step improves accuracy and quality of the finished product. |
| Calibrating | A finishing operation that brings the forging to precise dimensions. The workpiece is placed in a calibration die, where under pressure its surface is leveled and the geometry is brought to the specified tolerances. This process eliminates minor shape distortions left after previous operations. As a result, the part receives stable dimensions and a smooth surface without additional machining. |