






Mechanical press Sangiacomo T.450 RCE — 450 ton
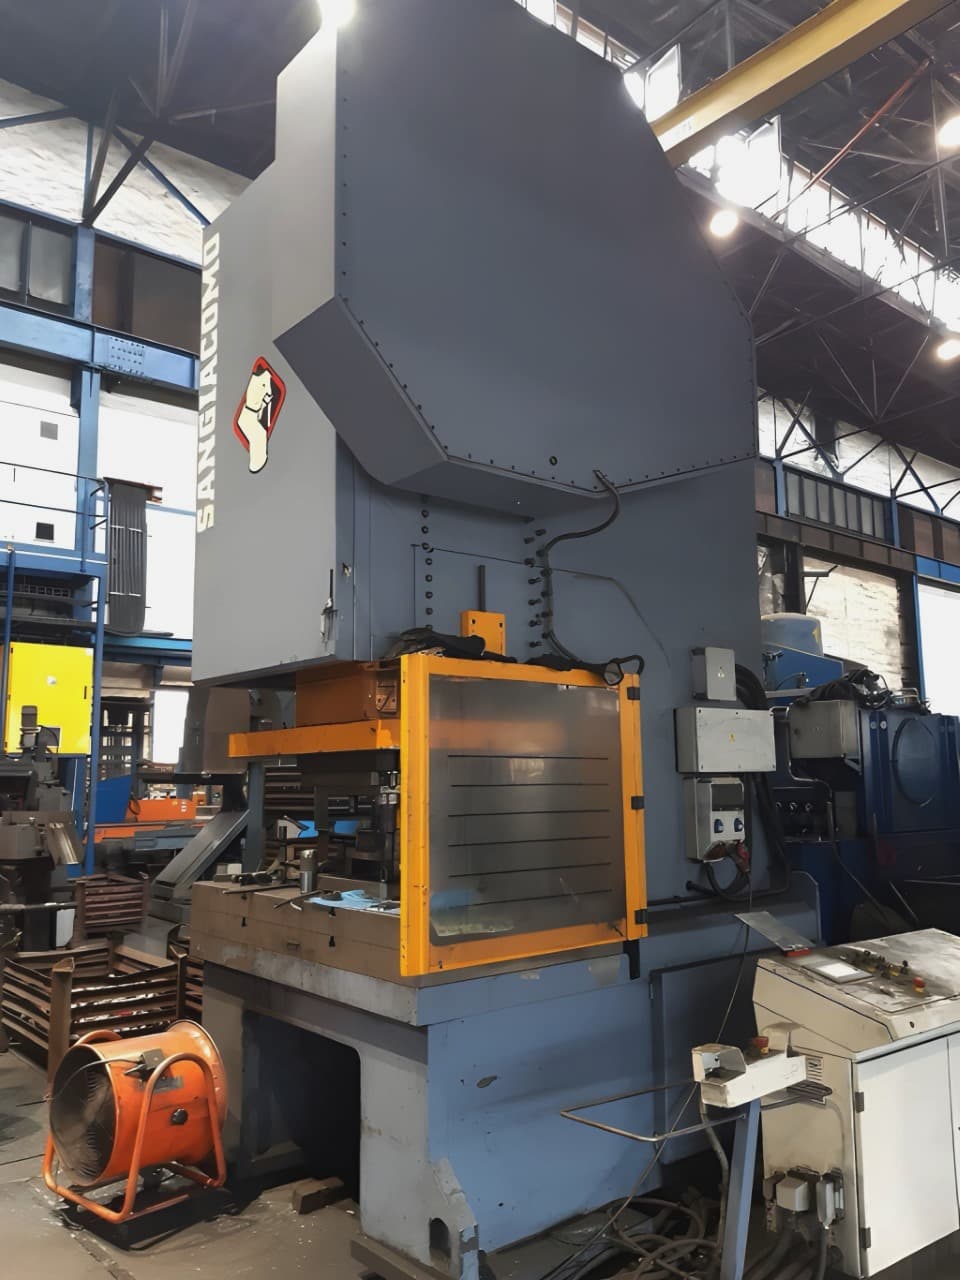
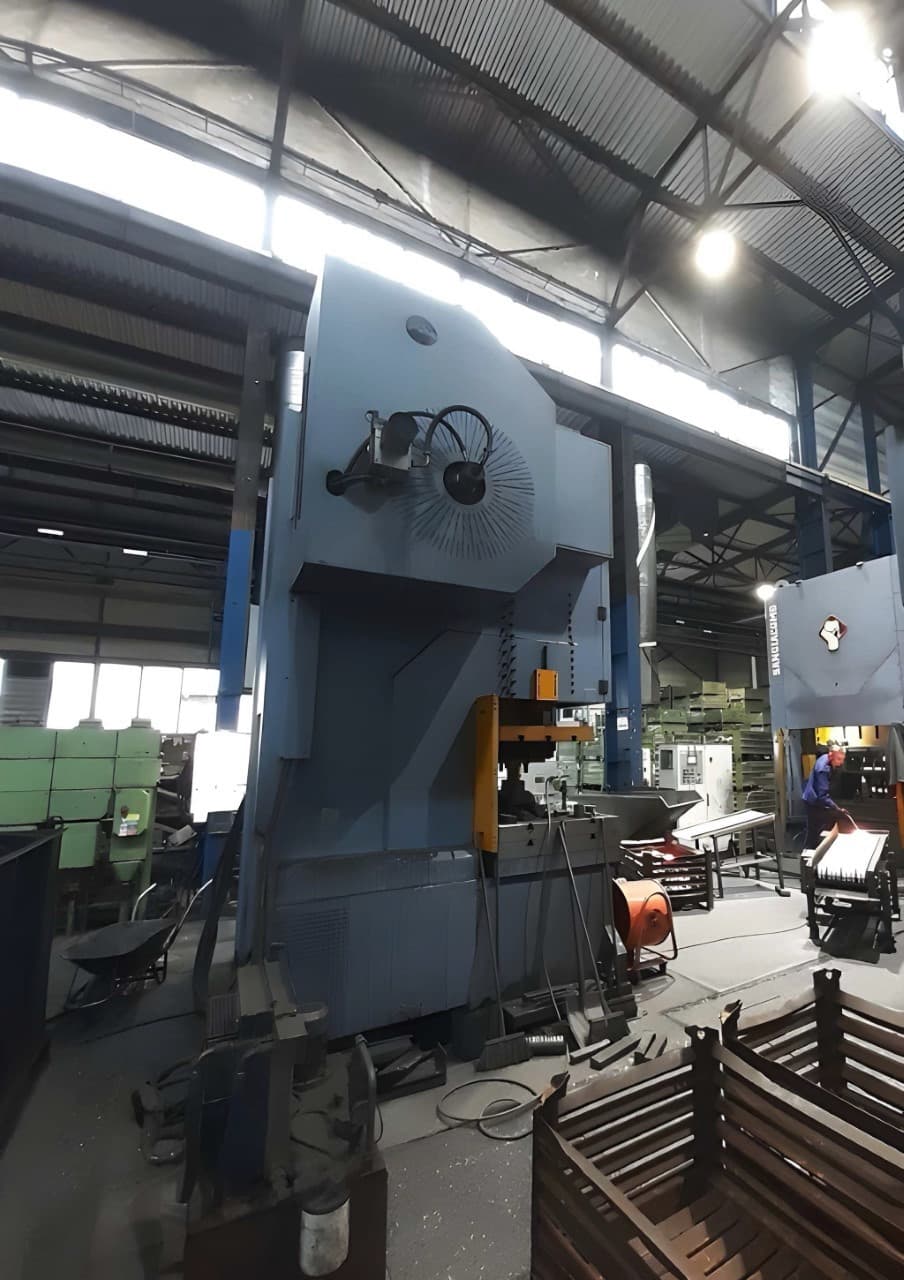
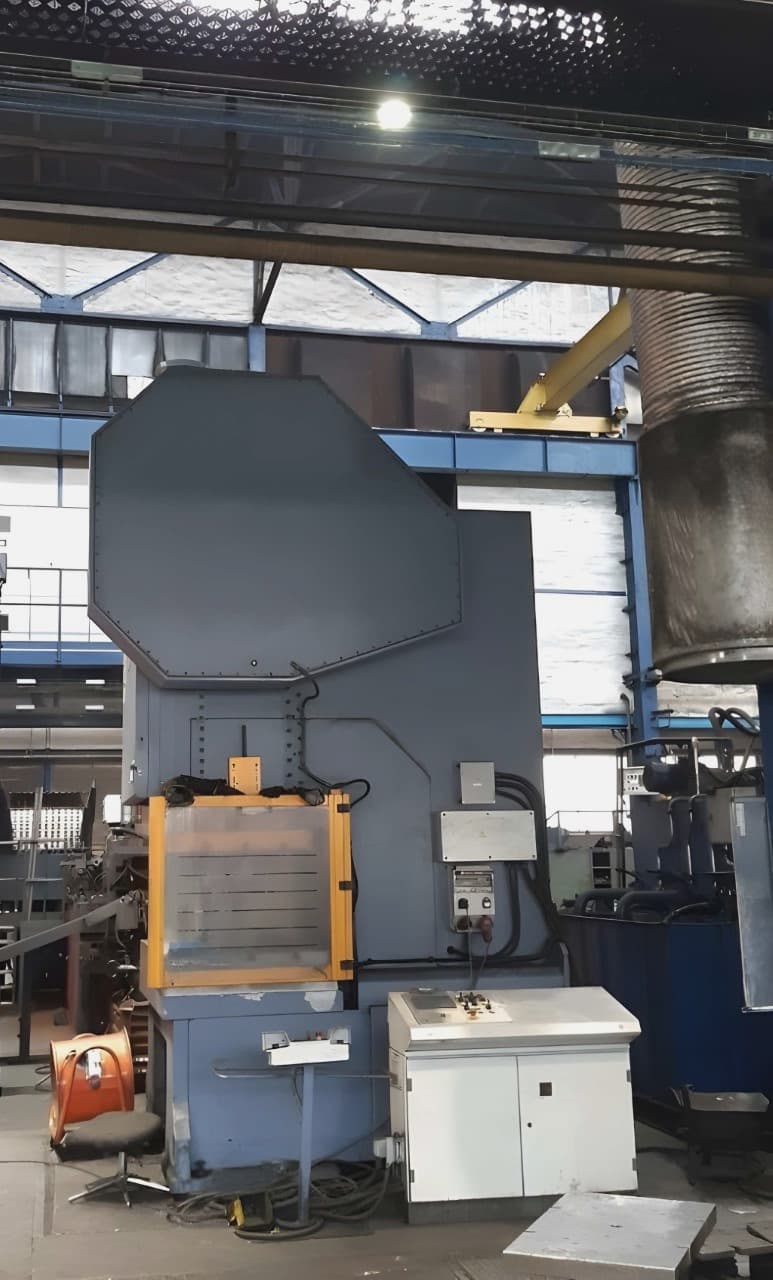
Sangiacomo T.450 RCE c-type press - description
Sangiacomo T.450 RCE video (ID:76536)
Technical specifications Sangiacomo T.450 RCE (ID:76536)
| Type | C-type press |
|---|---|
| Manufacturer | Sangiacomo |
| Model | T.450 RCE |
| Year of manufacture | 2018 |
| Nominal force | 4500 kN / 450 ton |
| Strokes per minute | 34 |
| Stroke | 22 - 250 mm |
| Table dimensions | 1000 x 1800 mm |
| Ram size | 900 x 1400 mm |
| Ram adjustment | 120 mm |
| Max die surface | 900 x 1650 mm |
| Max upper die weight | 900 kg |
| Machine depth | 3100 mm |
| Machine height | 4900 mm |
| Mass | 50000 kg |
Please note: Specifications are indicative and subject to final confirmation. For current availability and price, as well as photos and technical details, please contact us.
C-type press Sangiacomo - technological processes and operations
| Trimming | When a hot forging leaves the die, flash comes out with it — excess metal squeezed into the gap between the tools. It is removed on a trimming press, where the part passes through a die and the cutting edge shears off everything excess along the contour. This is how the forging gets a clean edge and precise shape, ready for the next stage. |
|---|---|
| Sheet stamping | Sheet stamping is a class of operations for forming parts from sheet material using dies. The workpiece is deformed in the tool without significant change in thickness, acquiring the specified shape. This group includes blanking, punching, bending, drawing, and other processes performed on presses. Sheet stamping is the foundation of mass production of body panels, housings, and other thin metal parts. |
| Punching | Punching holes in sheet metal is performed in a die: a tool with sharp edges passes through the workpiece, separating material along a closed contour. The process is fast and precise, leaving no burrs when properly set up. Used for producing holes, slots, and cutouts in sheet metal parts. |
| Blanking | Blanking a part from a sheet along a closed contour is performed on a press using a blanking die. The tool passes through the material, separating the finished part from the sheet. The accuracy of the contour and the cleanliness of the edge determine the quality of the final product. |
| Bending | Bending gives a sheet blank an angle or curvature. The metal is bent in the die under the force of the press: the outer layers stretch, the inner layers compress, and the middle retains its original length. The operation allows producing parts with the specified geometry without changing the material thickness. |
| Cutting | Separation of material into parts using a cutting tool. Depending on the task, cutting is performed on presses, shears, or special machines, separating the workpiece from a sheet, strip, or bar. The operation provides workpieces of the required size for subsequent forming. |