






Forging hammer Huta Zygmunt MPM 1600 B — 1840 kgm

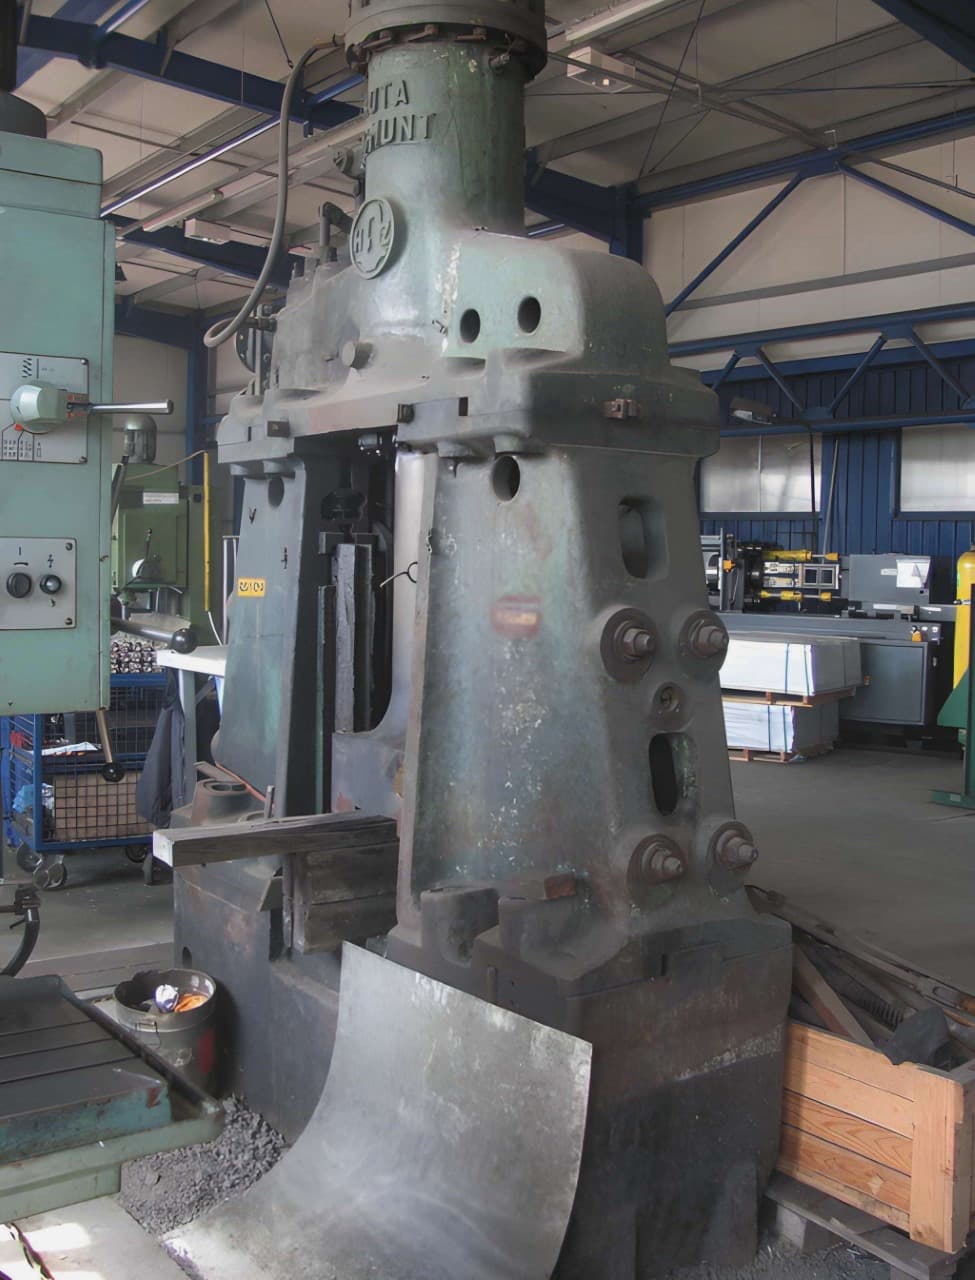
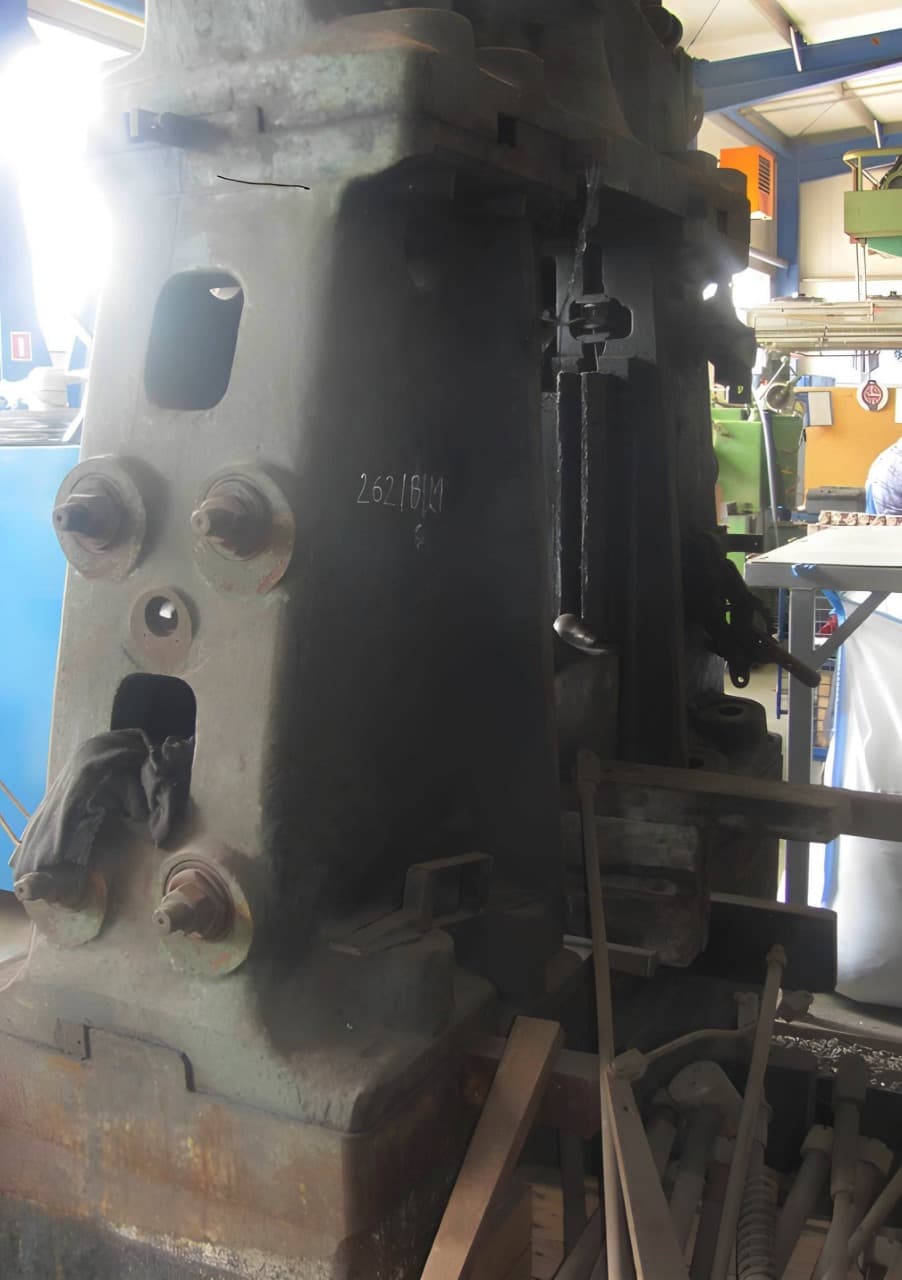
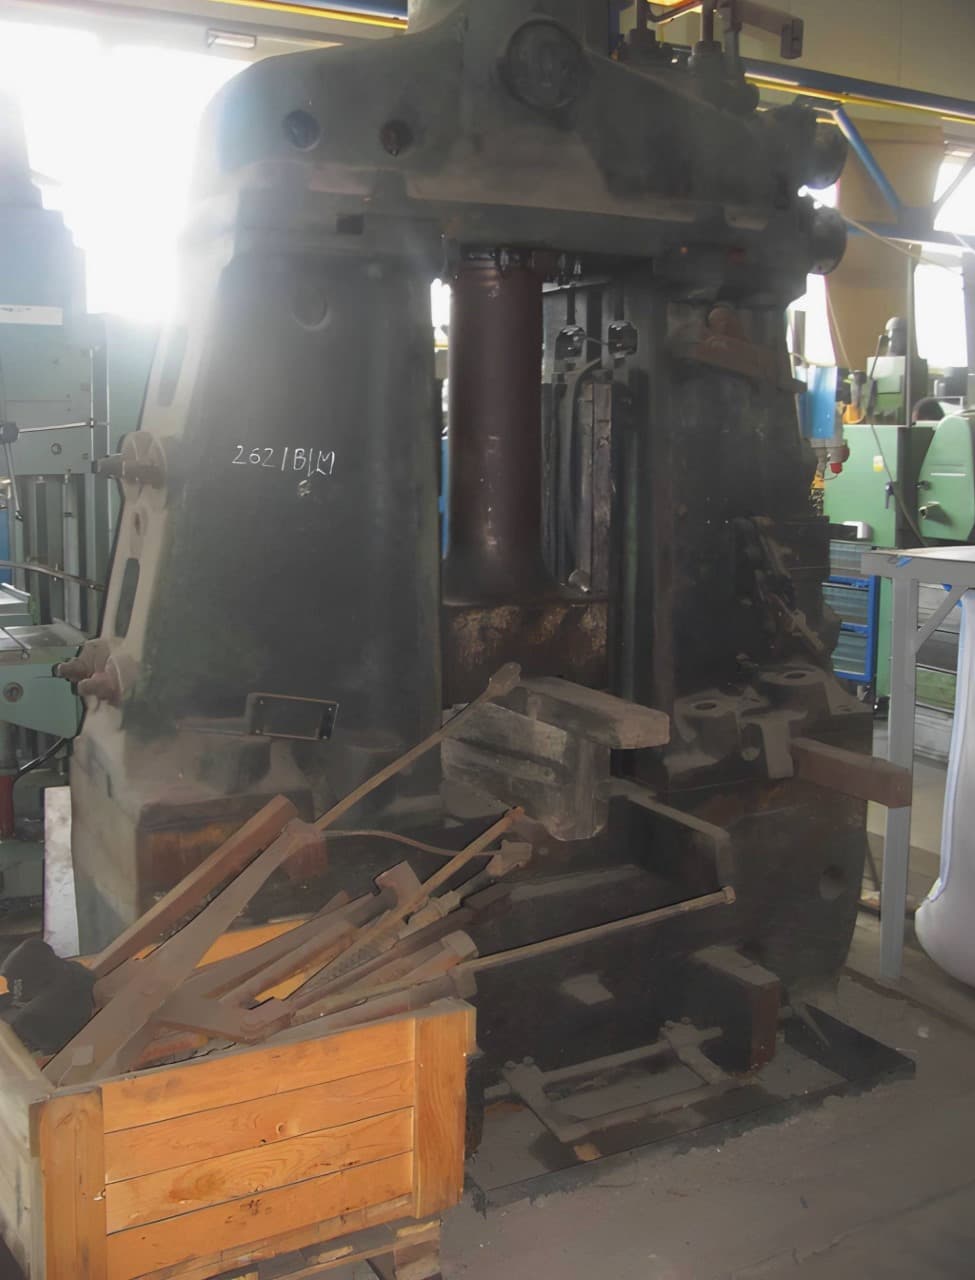
Huta Zygmunt MPM 1600 B forging hammer - description
Technical specifications Huta Zygmunt MPM 1600 B (ID:S93428)
| Type | Forging hammer |
|---|---|
| Manufacturer | Huta Zygmunt |
| Model | MPM 1600 B |
| Blow energy | 1840 kgm |
| Weight of falling parts | 630 kg |
| Stroke | 750 mm |
| Opening between the stands | 430 mm |
| Length of die seat in falling parts | 400 mm |
| Length of die seat in bolster | 600 mm |
| Minimum die height | 180 mm |
| Maximum weight of upper die | 200 kg |
| Height of die parting line above floor | 800 mm |
| Blow per minute | 120 |
| Inlet air pressure | 0,5–0,7 MPa |
| Inlet steam pressure | 0,5–0,7 MPa |
| Average air consumption per minute | 7 m3 |
| Average steam consumption per hour | 380 kg |
| Cylinder diameter | 320 mm |
| Falling parts rod diameter | 240 mm |
| Inlet pipe diameter | 80 mm |
| Outlet pipe diameter | 80 mm |
| Anvil weight | 12500 kg |
| Total weight | 21900 kg |
Forging hammer Huta Zygmunt - technological processes and operations
| Forging | The process of plastic deformation of metal, in which the workpiece changes shape under the impact of blows or static pressure. During forging, the metal structure is densified, internal inhomogeneities are eliminated, and the mechanical properties of the material are improved. As a result, forged products are distinguished by high strength and reliability when operating under significant loads. Forging is used both for producing finished parts and for preparing workpieces for subsequent stamping. |
|---|---|
| Hot forging | Hot forging is a process of shaping metal under pressure at elevated temperatures. Heating reduces the deformation resistance of the material, allowing it to flow more easily into the die cavity. The process provides high productivity and the ability to form complex shapes. Used for manufacturing forgings from steel and alloys in series and mass production. |
| Closed-die forging | The workpiece is deformed inside a die cavity that restricts metal flow, forcing it to fill the exact shape of the tool. Under high pressure, the material spreads into every recess and detail of the die, producing a part with precise geometry. This method provides high accuracy and repeatability, making it the standard for series and mass production of complex forgings. |
| Drop forging | A method of hot closed-die forging in which the workpiece is deformed by the energy of a falling ram. Under the impact, the metal fills the die cavity, reproducing its geometry and taking the shape of the finished part. The process is characterized by high productivity and repeatability, making it in demand in series and mass production. |